When selecting, accepting, and maintaining laser equipment, two metrics are most frequently referenced yet commonly misunderstood: laser power and the beam quality factor M².
Power defines how much work the laser can process, while M² defines how finely the laser can process. Evaluating only power without checking M² may lead to processing results far below expectations; focusing solely on M² without sufficient power will result in insufficient productivity. Accurate measurement and interpretation of these two parameters are fundamental for equipment acceptance and process optimization.
This article explains the testing principles, methodologies, common measurement errors, and combined testing strategies for laser power and M² factor in full detail.
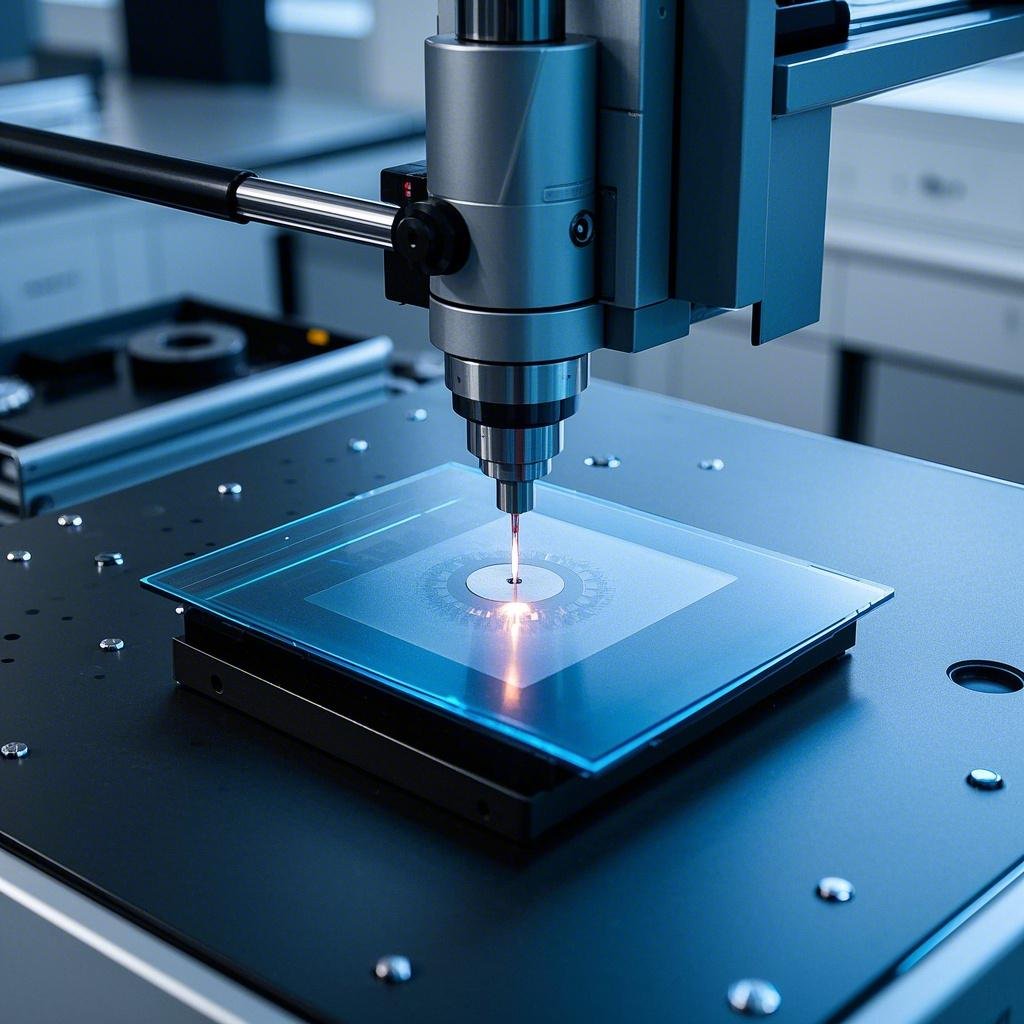
01 Laser Power Testing: Principles, Methods and Error Control
Three Core Measurement Methods
Laser power measurement essentially converts light energy into quantifiable thermal, electrical or mechanical signals. Three mainstream approaches are widely adopted:
Calorimetric Method: The absorber captures laser energy, and power is calculated from temperature rise. Suitable for long-duration measurement of high-power lasers.
Photovoltaic Method: A photodetector converts optical signals into electrical signals. Ideal for medium & low-power scenarios requiring fast response.
Integrating Sphere Method: Uniform absorption is achieved through multiple internal reflections. Designed for low-power lasers covering a broad wavelength range.
Common Pitfalls to Avoid
Wavelength Matching: Detector responsivity varies with wavelength. Probes must be matched to the laser wavelength; otherwise, significant reading deviation will occur.
Power Density Tolerance: High power density may damage probes. Attenuators or beam splitters should be applied when necessary.
Ambient Temperature & Cooling: Thermal drift must be considered for extended measurement. Water-cooled power meters are preferred for industrial on-site applications.
Beam Size and Position: The probe aperture must exceed the beam size. Partial beam clipping at the edge will produce underreadings.
Engineering Recommendations
For industrial laser equipment, a hybrid approach of on-line power monitoring + periodic off-line calibration is recommended. On-line monitoring detects power attenuation promptly, while off-line calibration guarantees metrological traceability.
02 M² Factor Testing: From Definition to Practical Implementation
Physical Meaning of M²
M² is defined as the ratio between the product of beam waist radius and far-field divergence angle of an actual beam, and the corresponding value of an ideal fundamental-mode Gaussian beam.
An ideal Gaussian beam has M² = 1, while real lasers have M² ≥ 1. The closer M² is to 1, the better the beam quality and the stronger the focusing capability.
Testing Principles and Standards
M² measurement follows ISO 11146. The core procedure is to measure beam spot sizes at multiple axial positions, fit a hyperbola to determine the beam waist location, waist radius and divergence angle, then compute the M² value.
Key steps:
Measure spot sizes at different positions using CCD camera or knife-edge scanning method
Measurement range must cover at least one Rayleigh length before and after the beam waist
Apply hyperbolic fitting instead of simple linear fitting to reduce errors
Common Sources of Uncertainty
Optical aberration: Lenses and mirrors in the test setup introduce extra aberration and inflate M² readings
Camera saturation and non-linearity: Saturated beam center severely distorts beam width calculation
Background noise: Dark-field subtraction and threshold processing are required
Mechanical positioning accuracy: Precision of the translation stage directly affects fitting reliability
03 Combined Testing Strategy for Power and M²
Power and M² are not independent during real-world testing. Thermal deformation of optical components under high operating power can degrade beam quality. Recommended practice:
Measure M² at low power as the baseline reference
Ramp up to working power, wait for thermal equilibrium, then re-test M² to evaluate thermally induced beam quality degradation
Record power and M² changes over time simultaneously to assess equipment stability
For high-power lasers, use beam sampling via beam splitter to prevent instrument damage from direct exposure
04 Test Report and Result Interpretation
A complete test report shall include:
Test conditions (power, wavelength, ambient temperature)
Test instruments and calibration status
Raw measurement data and fitting curves
M² value and measurement uncertainty
Laser power value and fluctuation range
Interpretation notes: M² typically carries relatively large measurement uncertainty. When comparing data across different devices, focus on trends rather than absolute values. For power measurement, long-term stability and repeatability are the key concerns.
05 Our Testing Services
As an accredited third-party laser testing laboratory, we provide full-suite laser power and M² testing services:
Laser power testing: Coverage from pW up to 5 kW, supporting calorimetric, photovoltaic and integrating sphere methods
M² testing: Compliant with ISO 11146, using CCD camera and precision translation stage with hyperbolic curve fitting
Combined testing: Low-power baseline measurement + re-test at operating power to assess thermal beam quality degradation
Test report issuance: Including test conditions, raw data, fitting curves and uncertainty analysis
End-to-end service: Custom test scheme development, sample measurement and report interpretation, all in one package
Custom consultation: If you are unsure which tests your laser equipment requires or how to interpret M² results, send us your datasheet. Our engineers will tailor a dedicated testing plan for you.